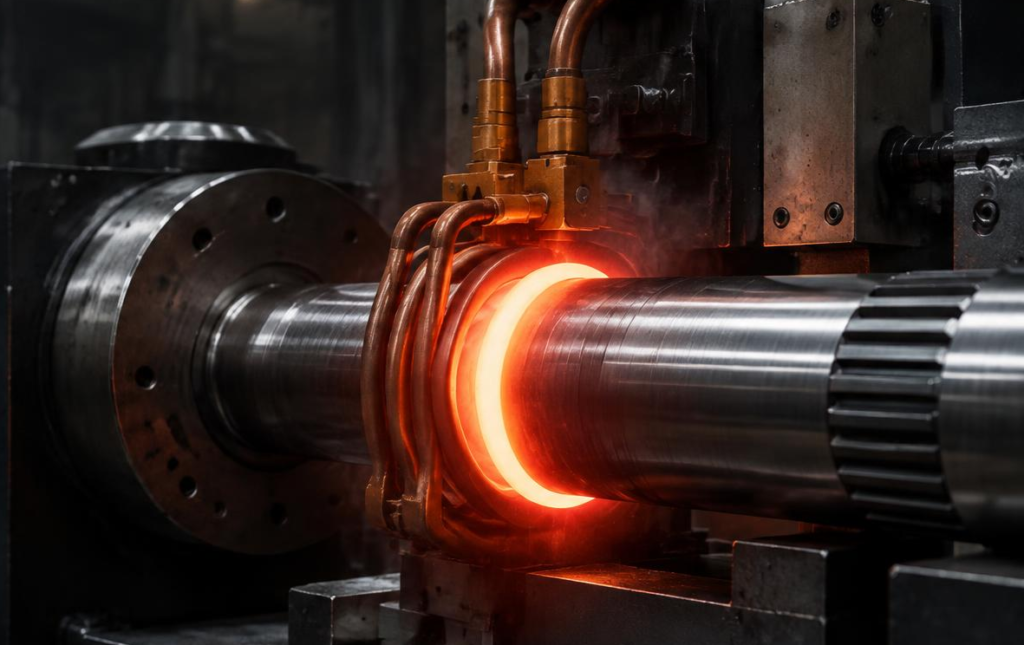
Induction hardening is a surface hardening process that heats the outer layer of steel with induced electric current, then immediately cools it with a spray of water or polymer solution. The surface transforms into hard martensite, while the core never gets hot enough to change and stays tough. The whole cycle takes only seconds, which makes it the first choice for shafts, gears, and crankshafts made in high volumes.
Induction hardening belongs to the thermal family of surface hardening methods, alongside flame hardening and laser hardening. This guide explains the working principle, how frequency controls case depth, the process steps, techniques and coils, suitable steels, how case depth is measured, and then flame hardening and how the two compare.
What Is Induction Hardening?
Induction hardening is a heat treatment that hardens only the surface of a part without changing its chemical composition. That is the key difference from diffusion methods such as carburizing and nitriding, which add carbon or nitrogen to the surface.
Because nothing is added, the steel must already contain enough carbon to harden, usually about 0.35–0.55% C. The hardening principle is the same as ordinary quenching and tempering. The difference is that only the skin is heated, and much faster.
Typical results:
- Case depth: about 0.5–6 mm (0.02–0.24 in), controlled mainly by frequency.
- Surface hardness: about 50–60 HRC, depending on the steel’s carbon content.
- Core: stays in its original condition, usually quenched and tempered or normalized.
How Induction Hardening Works
Eddy currents and hysteresis
The part sits inside or near a copper coil carrying high-frequency alternating current. The current creates a changing magnetic field, which induces eddy currents in the steel. The steel’s electrical resistance to these currents generates heat. While the steel is still magnetic, the constant reversal of magnetization (hysteresis) adds a little more heat.
The principle is the same as an induction melting furnace. The difference is that in induction hardening, heating stops as soon as the surface reaches the austenite range.
The skin effect
Alternating current does not spread evenly through a metal cross-section. It crowds toward the surface, and the higher the frequency, the thinner the layer that carries it. This is the skin effect, and it is what lets induction hardening heat only the surface.
The depth in which most of the current flows is called the penetration depth (δ). For hot steel above the Curie point, a practical estimate is:
δ (mm) ≈ 500 / √f, with f in hertz.
For example, at 10 kHz the penetration depth is about 5 mm, and at 400 kHz about 0.8 mm.
The Curie point
Steel stays magnetic up to about 770 °C (1,420 °F), the Curie point. Above it, steel loses its magnetism, hysteresis stops, and the penetration depth increases several times over. Heating becomes less efficient past this point, so induction machines are designed with enough power to get through it quickly.
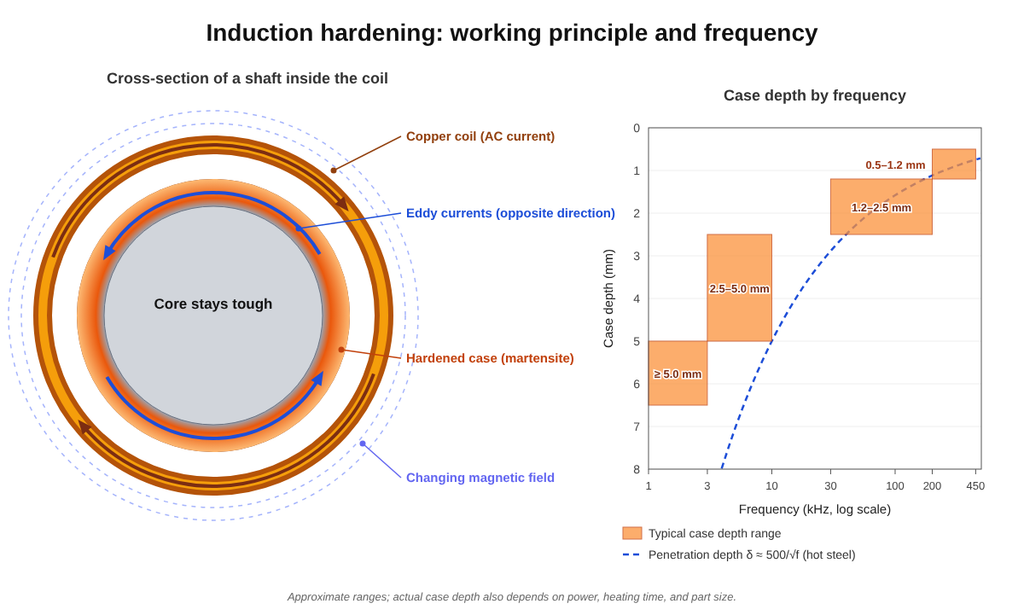
The diagram above shows the coil current, the opposing eddy currents at the shaft surface, and the case that hardens after quenching. The chart beside it shows the typical case depth range for each frequency band.
Frequency and Case Depth
Frequency is the main control for case depth in induction hardening. The hardened case is usually shallower than the penetration depth, because heat also conducts inward and the quench begins before the whole penetration layer reaches austenite.
| Frequency | Case depth (approx.) | Typical parts |
|---|---|---|
| 200–450 kHz | 0.5–1.2 mm | Small pins, fine-pitch gears, cutting edges |
| 30–200 kHz | 1.2–2.5 mm | Small to medium shafts, sprockets |
| 3–10 kHz | 2.5–5 mm | Large shafts, crankshafts, large gears |
| 1–3 kHz | 5 mm or more | Rolls, large-diameter shafts |
These are general ranges. Besides frequency, case depth also depends on:
- Power and heating time. High power for a short time gives a thin case with a sharp boundary. Lower power for longer lets heat conduct inward, giving a deeper case with a more gradual transition.
- Scan speed in progressive hardening.
- Part diameter. On small shafts, a frequency that is too low can heat the whole cross-section, so the core hardens too.
As a rough guide to choosing frequency, pick one whose penetration depth is about 1.5–2 times the case depth you want. The exact setting is still confirmed by trial runs and sectioning.
The Induction Hardening Process, Step by Step
1. Prepare the material
The starting microstructure matters a great deal. Because heating lasts only seconds, carbon must dissolve into austenite quickly. A fine, uniform structure, such as quenched and tempered or normalized steel, gives more even hardness than coarse pearlite or banded ferrite.
2. Heat
The surface is heated into the austenite range, usually about 850–1,000 °C (1,560–1,830 °F). This is higher than normal furnace hardening temperatures, because the time is so short that carbon needs the extra temperature to dissolve. Heating usually takes a few seconds to a few tens of seconds. Going too hot coarsens the grain and raises the risk of cracking.
3. Quench
As soon as temperature is reached, the surface is sprayed with quenchant. This step is called induction quenching. Common media:
- Water: the fastest cooling and highest hardness, but also the highest cracking risk.
- Polymer solution (such as PAG): the cooling rate is adjusted by concentration. This is the most common choice for alloy steels such as 4140 and crack-prone shapes.
- Oil or air: for high-hardenability steels such as tool steels.
4. Temper
As-quenched martensite is very hard but brittle, so parts are almost always tempered at about 150–200 °C (300–390 °F). Tempering can be done in an ordinary furnace, or with a second induction coil on the same line. The second option is called induction tempering, and it takes only seconds to minutes. Tempering should follow the quench promptly, because residual stress can cause delayed cracking.
Induction Hardening Techniques
Single shot
The whole area to be hardened is heated at once, then quenched. The part is usually rotated so heating is even. This suits short parts such as pins, bearing seats, and shaft ends.
Scanning (progressive)
The coil and quench spray travel slowly along the part, or the part moves through the coil. The freshly heated zone is sprayed right behind the coil. This technique is used for long shafts, piston rods, and induction hardened chrome shafting (hydraulic rods that are induction hardened and then chrome plated).
Gears
- Spin hardening: the whole gear rotates inside a ring coil and is heated at once. Suits small to medium gears.
- Tooth-by-tooth or gap-by-gap: a shaped coil hardens one tooth or one gap per pass. Used for large gears that cannot be heated all at once.
Shafts and crankshafts
On shafts, induction hardening is usually applied to bearing seats, splines, and areas under torsion. On crankshafts, the main and pin journals are hardened one at a time with half-ring coils that ride on the rotating journal. The fillet radii are often hardened too, to raise fatigue strength.
Coils (Inductors) and Coil Design
The coil, or inductor, is usually made from water-cooled copper tubing. Its shape follows the area to be hardened, so coil design largely decides how uniform the result is:
- A small coupling gap between coil and part gives high efficiency, usually a few millimeters. An uneven gap gives uneven heating.
- Flux concentrators made of soft magnetic material are fitted to the coil to steer the field toward specific areas, such as crankshaft fillets.
- Sharp corners, holes, and keyways tend to overheat because current crowds there. Coil design and process settings have to allow for this.
Because every part shape needs its own coil, induction hardening is most economical in high-volume production.
Steels and Cast Irons for Induction Hardening
| Material | Examples | Surface hardness (approx.) | Notes |
|---|---|---|---|
| Medium-carbon steel | 1045 / C45, 1050, 1055 | 55–60 HRC | Most common and lowest cost |
| Cr-Mo alloy steel | 4140 / 42CrMo4, 4340 | 52–58 HRC | Stronger core; polymer quench |
| High-carbon steel | 1060, spring and bearing steels | 58–63 HRC | Crack-prone; milder quench |
| Martensitic stainless | 410, 420, 440C | 45–58 HRC | Austenitic grades (304, 316) cannot be hardened |
| Ductile iron | 80-55-06, 100-70-03 | 50–56 HRC | Matrix must be pearlitic |
| Gray cast iron | Class 35, Class 40 | 45–52 HRC | Pearlitic matrix; machine ways, liners |
Hardness by carbon content
Surface hardness after induction hardening depends mainly on carbon content, not alloying elements. Alloying elements matter more for hardenability and core strength. Approximate hardness after quenching and a light temper:
| Carbon content | Example steel | Surface hardness (approx.) |
|---|---|---|
| 0.30% | 1030 | 45–50 HRC |
| 0.40% | 1040, 4140 | 52–57 HRC |
| 0.45% | 1045 | 55–59 HRC |
| 0.50–0.55% | 1050, 1055 | 57–61 HRC |
| 0.60% | 1060 | 59–63 HRC |
Induction hardening 1045 and 4140
1045 (equivalent to C45 and S45C) is the steel most often induction hardened. Its carbon content is right for about 55–59 HRC, it is cheap, and it machines easily. Because its hardenability is low, it is usually quenched in water or a dilute polymer.
4140 (equivalent to 42CrMo4 and SCM440) is used when the core must be stronger and tougher, for example on shafts carrying high torsional loads. It is usually quenched and tempered before induction hardening, giving a core of about 28–32 HRC. Its surface hardness is slightly lower than 1045’s, about 52–57 HRC, because it contains 0.40% carbon.
Ductile and gray cast iron
Ductile iron and gray cast iron can be induction hardened as long as the matrix is pearlitic. A ferritic matrix lacks enough dissolved carbon to form martensite in such a short heating time. Uses include ductile iron crankshafts, machine tool guideways, and cylinder liners.
What about low-carbon steel and stainless steel?
Low carbon steel such as 1018 or A36 cannot be meaningfully induction hardened, because it has too little carbon to form hard martensite. For these steels, carburizing is the answer. Martensitic stainless steels (410, 420, 440C) can be induction hardened, but austenitic grades such as 304 and 316 cannot, because they do not transform to martensite.
Case Depth in Induction Hardening and How It Is Measured
In induction hardening, the effective case depth is the distance from the surface to the point where hardness drops to a set limit. Under ISO 18203, the limit is usually 80% of the minimum required surface hardness (in HV). For example, if the minimum surface hardness is 600 HV, the limit is 480 HV.
How it is measured:
- Cut the part perpendicular to the surface, then polish and etch the section.
- Take Vickers microhardness readings at set intervals from the surface toward the core.
- Plot the hardness profile and read the depth where it crosses the limit hardness.
An induction-hardened case also shows clearly after a nital etch, so quick checks on the shop floor often use a visual measurement on an etched section. Non-destructive methods such as ultrasonic and eddy current testing exist, but they still need calibrating against sections.
Flame Hardening
What is flame hardening?
Flame hardening is a surface hardening method that uses a gas flame as the heat source. An oxyacetylene or oxy-propane flame is played on the surface until it reaches the austenite range, then the surface is sprayed with water immediately. The metallurgy is exactly the same as induction hardening. Only the heat source differs.
The flame hardening process and temperature
An oxyacetylene flame reaches about 3,100 °C (5,600 °F) at the tip of its inner cone, so the steel surface can be brought to about 850–950 °C (1,560–1,740 °F) quickly. The burner and the water spray are usually mounted close together, with the burner leading and the spray following. Case depth is controlled by burner travel speed, flame-to-surface distance, and gas mixture. Typical case depth is about 1.5–6 mm (0.06–0.24 in).
Types of flame hardening
- Stationary (spot): burner and part stay still; a small area is heated and quenched. Used for lever ends, valve seats, and other small areas.
- Progressive: the burner and spray travel in a straight line along the part. Used for machine guideways, blades, and long flat surfaces.
- Spinning: the part rotates in front of a fixed burner, then its whole circumference is quenched at once. Used for small gears, rolls, and short shafts.
- Progressive-spinning: the part rotates while the burner travels along its axis. Used for long shafts and rolls.
Steels for flame hardening
The materials are the same as for induction hardening: medium-carbon steels such as 1045, alloy steels such as 4140, and pearlitic gray and ductile irons. Tool steels can also be flame hardened, for example on the cutting edges of large dies. Air-hardening tool steels such as A2, and to a degree D2, only need to cool in still air after heating, so the cracking risk is lower. D2 needs a higher hardening temperature, so heating has to be controlled more carefully.
Advantages and disadvantages of flame hardening
Advantages:
- Simple, inexpensive, portable equipment.
- Suits very large parts that will not fit an induction machine, such as gears several meters across and steel mill rolls.
- Economical for one or a few parts, because no dedicated coil is needed.
Disadvantages:
- Less precise temperature control, so results depend more on operator skill.
- Heating can be less even, with a risk of scorching or overheating.
- Slower and less energy-efficient than induction.
Induction Hardening vs. Flame Hardening
| Aspect | Induction hardening | Flame hardening |
|---|---|---|
| Heat source | Induced current from a coil | Gas flame (oxyacetylene, oxy-propane) |
| Speed | Very fast, seconds | Slower |
| Temperature and depth control | Precise, easy to automate | Depends on the operator |
| Case depth | 0.5–6 mm | 1.5–6 mm |
| Equipment cost | High; one coil per part shape | Low; simple equipment |
| Best production volume | High volume | One-offs or small batches |
| Part size | Small to large | Ideal for very large parts |
| Energy efficiency | High; heat generated in the part | Low; much heat is lost |
| Distortion | Low to medium | Medium |
In short, induction hardening is chosen for high-volume production that needs consistent results. Flame hardening is chosen for very large parts, field repairs, or quantities too small to justify a dedicated coil.
Induction Hardening vs. Carburizing vs. Nitriding
| Aspect | Induction hardening | Carburizing | Nitriding (gas) |
|---|---|---|---|
| Principle | Thermal; composition unchanged | Carbon diffusion | Nitrogen diffusion |
| Process temperature | Rapid austenitizing (850–1,000 °C / 1,560–1,830 °F) | 850–950 °C (1,560–1,740 °F) | 500–550 °C (930–1,020 °F) |
| Quench | Yes | Yes | No |
| Case depth | 0.5–6 mm | 0.5–2 mm | 0.1–0.6 mm |
| Surface hardness | 50–60 HRC | 58–64 HRC | 600–1,100 HV |
| Suitable steels | Medium-carbon steels, cast irons | Low-carbon steels | Cr-Mo-Al alloy steels |
| Cycle time | Seconds | Several hours | 10–60+ hours |
| Selective hardening | Easy | Needs masking | Needs masking |
Induction hardening wins on speed, case depth, and ease of hardening only selected areas. Carburizing gives a harder surface on low-carbon steels. Nitriding gives the least distortion and the highest hardness, but a thin case.
Common Induction Hardening Problems
- Quench cracking: often at hole edges, keyways, sharp corners, or in steels with too much carbon quenched in water. Prevent with generous radii, a polymer quench, and prompt tempering.
- Overheating at edges and holes: current crowds there, so these areas can partially melt or coarsen.
- Soft spots: uneven quench spray, blocked nozzles, or scale and oil on the surface.
- Soft transition zone: at the end of a hardened area, or where two hardened areas meet, a zone gets tempered back, leaving it softer and holding tensile stress. This zone should not fall in a highly stressed region.
- Distortion: long shafts can bow. Usually handled by straightening or leaving grinding stock.
- Low or uneven hardness: a coarse starting structure, too low a temperature, or a delayed quench.
Fine quench cracks often only show up with non-destructive testing (NDT), especially magnetic particle inspection.
Applications of Induction and Flame Hardening
- Shafts and axles: transmission shafts, axles, pump shafts, and induction hardened shafts for linear bearings.
- Crankshafts and camshafts: journals and lobes, in both forged steel and ductile iron.
- Gears and sprockets: teeth hardened by spin or tooth-by-tooth methods.
- Piston rods and chrome shafting for hydraulic cylinders.
- Machine tool guideways, often in gray cast iron.
- Other automotive parts: CV joints, wheel hubs, and bearing seats. Examples are covered in our case study on metal casting in the automotive industry.
- Flame hardening: very large gears and sprockets, steel mill rolls, crane rails, excavator bucket teeth, and cutting edges of large dies.
Frequently Asked Questions
What is induction hardening? Induction hardening is a surface hardening process that heats the outer layer of steel with induced current from a coil, then immediately cools it with a water or polymer spray. The surface becomes hard martensite, while the core stays tough.
What is flame hardening? Flame hardening is surface hardening with a gas flame, usually oxyacetylene, that heats the steel surface into the austenite range before it is sprayed with water. It suits very large parts or small quantities.
What is the difference between induction hardening and flame hardening? Both heat the surface and then quench it. Induction hardening uses induced current, is faster and more precise, and suits high-volume production. Flame hardening uses a gas flame, needs simple equipment, and suits large parts or one-offs.
How does frequency affect case depth in induction hardening? The higher the frequency, the thinner the heated layer, because of the skin effect. Frequencies of a few hundred kHz give a case of about 0.5–1.2 mm, while a few kHz give 2.5–5 mm or more.
Which steels are suitable for induction hardening? Medium-carbon and alloy steels with about 0.35–0.55% carbon, such as 1045 and 4140, plus ductile and gray irons with a pearlitic matrix. Low-carbon steels should be carburized instead.
Related Articles
- Surface Hardening (Case Hardening): Methods, Comparison, and How to Choose
- Carburizing: Process Steps, Types, Case Depth, and Suitable Steels
- Nitriding: Process Steps, Types, Suitable Steels, and the White Layer
- Quenching and Tempering
- Types of Heat Treatment of Metals: Processes, Purposes, and Effects

Dagus R. Djuanda is a metallurgical engineer with more than 20 years of experience in materials engineering, specializing in magnetic materials. He holds a master’s degree in magnetic materials engineering, is a doctoral candidate in industrial engineering, and works as an engineer at the Ministry of Industry of the Republic of Indonesia. Founder of Metalurgika.