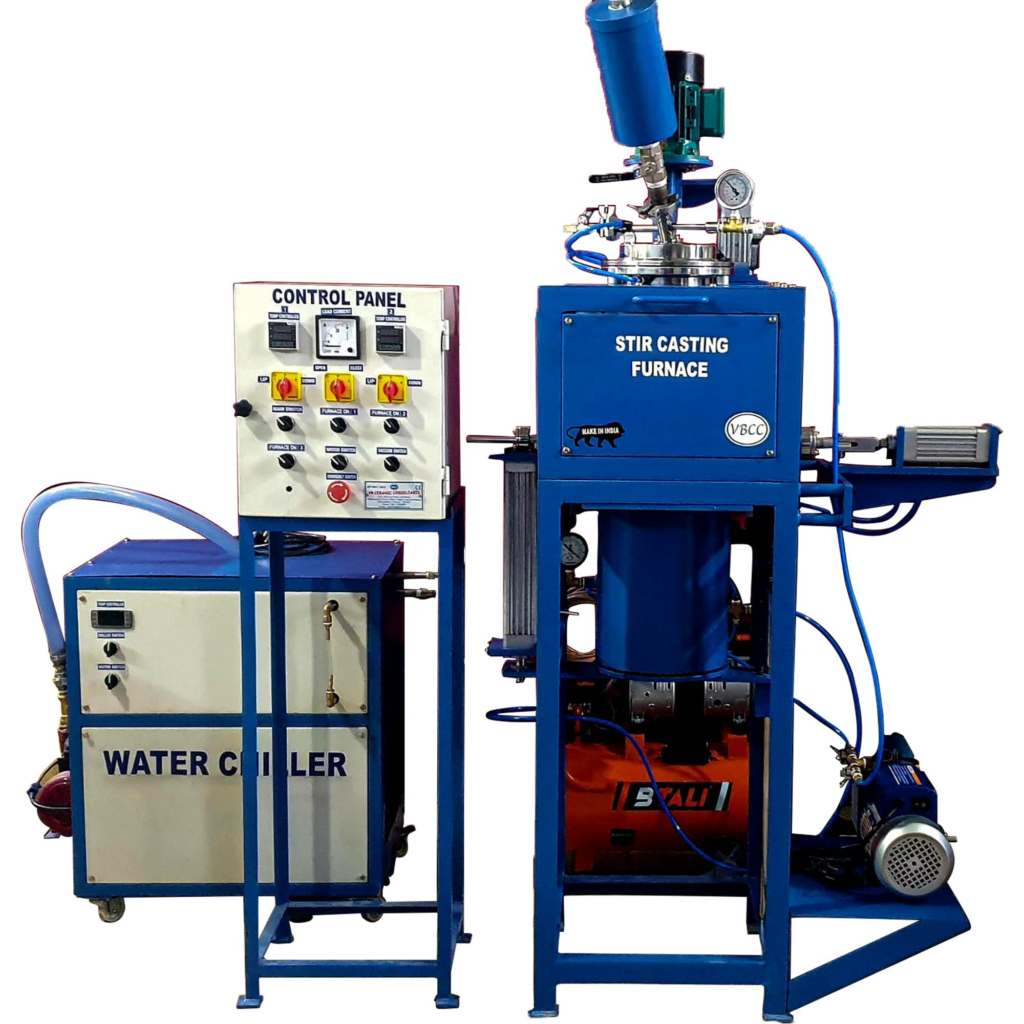
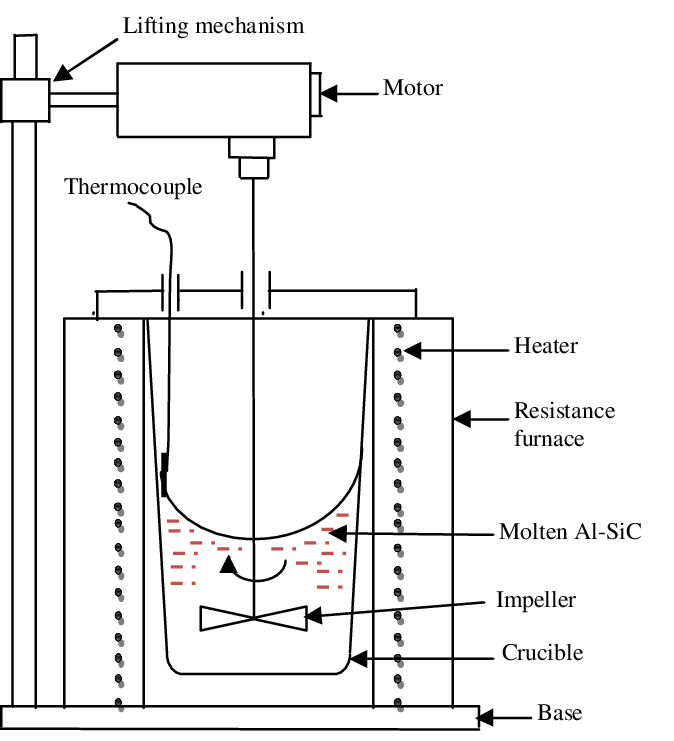
Stir casting is a method of making metal matrix composites by stirring reinforcement particles into molten metal and then pouring the mixture into a mold. A mechanical stirrer creates a vortex that draws the particles in and spreads them through the melt.
It is the simplest and cheapest liquid-state route to a metal matrix composite (MMC). That is why the stir casting process is the one most often used in university laboratories and in low-cost production of aluminum composites.
Materials Used in Stir Casting
Matrix. Aluminum alloys are by far the most common, especially aluminum-silicon casting alloys such as A356 and wrought alloys such as 6061. Magnesium and copper alloys are also used, but less often.
Reinforcement. Ceramic particles, usually a few micrometers to a few tens of micrometers in size:
- silicon carbide (SiC), the most widely used,
- alumina (Al₂O₃),
- boron carbide (B₄C),
- graphite, for self-lubricating properties,
- fly ash and rice husk ash, low-cost reinforcements that are widely studied.
The Stir Casting Process, Step by Step
1. Melt the matrix. The aluminum is melted in a crucible furnace and held above its liquidus, usually at about 700 to 800°C (1,290 to 1,470°F).
2. Clean the melt. Hydrogen is removed by degassing and the dross is skimmed off.
3. Preheat the reinforcement. The particles are heated to several hundred degrees to drive off moisture and adsorbed gas. Cold, damp particles are rejected by the melt and clump together.
4. Start stirring. The stirrer is lowered into the melt and turned until a vortex forms. Speeds reported in research are mostly in the range of 300 to 600 rpm.
5. Add the particles. The particles are fed slowly into the side of the vortex. Adding them all at once almost always produces clusters.
6. Keep stirring. Stirring continues for several minutes, typically 5 to 15, so the particles spread evenly.
7. Pour. The mixture is poured promptly into a preheated mold. Any delay gives the particles time to settle or float.
The temperatures, speeds, and times above are commonly reported ranges. The best values differ for each combination of matrix, particle, and crucible size.
Stir Casting Parameters That Decide the Result
| Parameter | If too low | If too high |
|---|---|---|
| Stirring speed | Particles are not drawn in and form clusters | Air is drawn in and porosity rises |
| Stirring time | Uneven distribution | More oxidation and interface reaction |
| Melt temperature | Melt is thick, hard to stir and pour | Particles react with the matrix, more dissolved gas |
| Particle preheat temperature | Melt rejects the particles | Particles oxidize too much |
| Reinforcement content | Little gain in properties | Melt becomes too thick, clustering |
The shape and position of the stirrer blades matter too. Angled blades placed about one third of the melt depth above the crucible floor are often used, so that particles at the bottom are lifted back into the flow.
Main Problems and How to Deal with Them
1. Poor wettability
Molten aluminum does not wet ceramic particles easily. The particles tend to be pushed out and float with the dross. Common remedies:
- add about 1% magnesium to lower the surface tension of the melt,
- preheat the particles before adding them,
- oxidize the SiC surface to form a thin silica layer,
- coat the particles with a metal such as nickel or copper.
2. Particle clustering
Fine particles stick together and form clusters, which become weak points in the casting. The smaller the particles, the worse the problem. It is reduced by slow feeding, two-step stirring, or ultrasonic vibration.
3. Settling
SiC has a density of about 3.2 g/cm³, against about 2.4 g/cm³ for molten aluminum, so the particles sink when the melt is left standing. The time between the end of stirring and pouring must be as short as possible.
4. Porosity
The vortex pulls air and gas into the melt. Porosity is reduced by moderate stirring speed, a protective gas atmosphere, and pressure during solidification, as in squeeze casting. How gas porosity forms in ordinary castings is covered in our case study on porosity and hot tearing.
5. Interface reaction
At high temperature and long contact time, SiC reacts with aluminum to form aluminum carbide (Al₄C₃), which is brittle and breaks down in moist air. Enough silicon in the matrix and a controlled melt temperature suppress this reaction.
Variants of Stir Casting
- Compocasting: the particles are stirred in while the metal is semi-solid. The thicker slurry holds the particles in place, so the distribution is better. The semi-solid state is explained in our article on semi-solid metal casting.
- Two-step stirring: the mixture is cooled to the semi-solid state, stirred, reheated, and stirred again before pouring.
- Bottom pouring: the crucible opens at the base, so the mixture drops straight into the mold with no delay. Many laboratory stir casting furnaces are built this way.
- Ultrasonic-assisted stir casting: vibration breaks up clusters, especially with nano-sized particles.
- Stir casting followed by squeeze casting: pressure during solidification closes the pores.
Advantages and Limitations
Advantages
- Simple, low-cost equipment.
- Works with ordinary foundry furnaces and molds.
- Easy to scale up, and suitable for complex casting shapes.
Limitations
- A truly even particle distribution is hard to achieve.
- Reinforcement content is limited, in practice to about 20 to 30% by volume.
- Porosity is higher than with powder metallurgy.
- Nano-sized particles are hard to disperse without extra equipment.
Where Stir Cast Composites Are Used
Aluminum-SiC composites made by stir casting are used or under development for brake discs, pistons, cylinder liners, and other parts that need high stiffness and wear resistance at low weight. For parts with the highest quality demands, industry more often chooses powder metallurgy or infiltration.
Frequently Asked Questions
How is stir casting different from ordinary casting? The pouring step is the same. The difference comes before pouring: in stir casting, reinforcement particles are stirred into the molten metal, so the result is a composite and not a plain alloy.
Why is magnesium added in stir casting? Magnesium lowers the surface tension of molten aluminum and reacts with the oxide layer, so the ceramic particles are wetted more easily and enter the melt.
Can stir cast composites be machined? Yes, but the hard ceramic particles wear cutting tools quickly. Polycrystalline diamond (PCD) tools are normally used.
What is the difference between stir casting and friction stir processing? They are unrelated. Stir casting mixes particles into liquid metal. Friction stir processing uses a rotating tool to mix particles into the surface of solid metal.
Conclusion
Stir casting is the cheapest way into metal matrix composites because it adds only one stirring step to an ordinary casting process. The quality of the result depends on how well wettability, clustering, settling, and porosity are controlled, and all four come down to particle preparation and to the temperature, speed, and time of stirring.
Related Articles
- Metal Matrix Composites (MMC): Applications and Production Challenges
- Semi-Solid Metal Casting Technology: Thixocasting and Rheocasting
- Nanostructured Materials in Metallurgy: Applications and Potential
- Metal Casting Defect Case Study: Porosity and Hot Tearing in Manufacturing
- Choosing Materials for Metal Casting: Cast Iron, Cast Steel, and Aluminum Alloys