
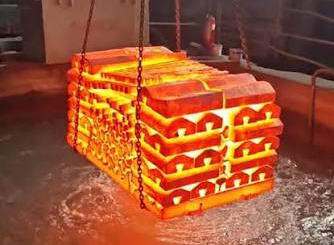
Quenching and tempering is a two-stage heat treatment that gives steel a combination of high strength and good toughness. The steel is first hardened by rapid cooling, then reheated to a lower temperature to reduce brittleness. Steel treated this way is called quenched and tempered, or Q&T, steel.
It is one of the main processes covered in our overview of the types of heat treatment of metals. This article looks at it in detail.
The Three Steps
1. Austenitizing
The steel is heated until its structure transforms to austenite, a phase that can dissolve carbon. For most medium-carbon and low-alloy steels this is roughly 815–870°C. The part is held long enough for the whole cross-section to reach temperature.
2. Quenching
The hot steel is cooled rapidly in a liquid or gas. If cooling is fast enough, the carbon has no time to diffuse out, and the austenite transforms to martensite. Martensite is very hard and strong, but also brittle and full of internal stress.
3. Tempering
The quenched steel is reheated to a temperature below its lower transformation point, typically between 150 and 650°C, held, and cooled. Tempering lets some carbon leave the martensite as fine carbides. Hardness drops somewhat, while toughness and ductility rise sharply.
Steel should be tempered soon after quenching. Untempered martensite left sitting under its own stress can crack.
Quenching Media
The quenchant sets the cooling rate. Faster is not always better: the goal is to cool just fast enough to form martensite, and no faster.
| Medium | Cooling severity | Typical use | Main risk |
|---|---|---|---|
| Brine (salt water) | Very high | Plain carbon steels, simple shapes | Cracking and distortion |
| Water | High | Low-hardenability carbon steels | Cracking in complex shapes |
| Polymer solution | Adjustable, between water and oil | Alloy steels, induction hardening | Concentration must be controlled |
| Oil | Moderate | Most alloy steels | Fire hazard, slower cooling |
| Molten salt | Moderate, very uniform | Martempering and austempering | Handling and safety |
| Gas or air | Low | Air-hardening tool steels, vacuum furnaces | Needs high-hardenability steel |
Hardenability: Why Alloy Content Matters
Hardness and hardenability are different properties.
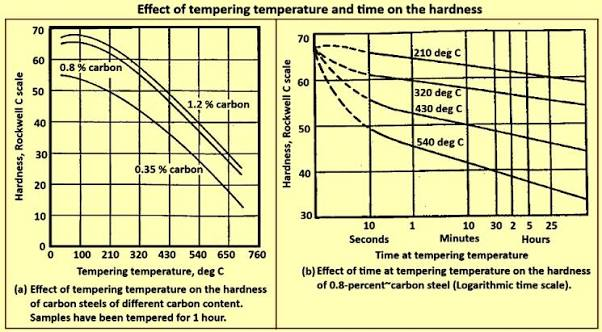
- Maximum hardness depends almost entirely on carbon content. A steel with about 0.4% carbon can reach the mid-to-high 50s HRC when fully martensitic, and steels above about 0.6% carbon can exceed 60 HRC.
- Hardenability is how deep that hardness reaches below the surface. It depends on alloying elements such as chromium, molybdenum, manganese, and nickel.
A thick bar of plain carbon steel may harden only at the surface, because the center cools too slowly. An alloy steel of the same size can harden all the way through, even in oil. Hardenability is measured with the Jominy end-quench test.
Tempering Temperature Ranges
| Range | Temperature | Result | Typical parts |
|---|---|---|---|
| Low | About 150–250°C | Highest hardness and wear resistance, stress relieved | Cutting tools, bearings, carburized gears |
| Medium | About 350–500°C | High elastic limit | Springs |
| High | About 500–650°C | Best toughness with good strength | Shafts, bolts, structural and pressure parts |
The higher the tempering temperature, the lower the hardness and the higher the toughness. Tempering time matters too, but temperature has by far the larger effect.
Temperatures to Avoid
- Tempered martensite embrittlement. Tempering in roughly the 250–400°C range can lower impact toughness even though hardness keeps falling. This range is normally avoided for parts that see shock loads.
- Temper embrittlement. Some alloy steels lose toughness if they are held in, or cooled slowly through, roughly 375–575°C. Impurities such as phosphorus, tin, and antimony are responsible. Cooling quickly after high-temperature tempering avoids it.
These ranges are approximate and vary by steel grade.
Common Problems and How to Prevent Them
| Problem | Cause | Prevention |
|---|---|---|
| Quench cracks | Cooling too severe, sharp corners, delayed tempering | Use a milder quenchant, add radii, temper promptly |
| Distortion | Uneven cooling, poor racking | Support parts properly, agitate the quenchant uniformly |
| Soft spots | Vapor pockets, scale, poor agitation | Clean parts, improve agitation |
| Low hardness | Under-heating, slow transfer to the quench | Verify furnace temperature, shorten transfer time |
| Retained austenite | High carbon or alloy content | Sub-zero treatment, double tempering |
| Decarburization | Surface carbon lost in the furnace | Use a protective atmosphere |
Hardness testing after tempering is the standard check that the treatment met its target.
Variations on the Process
- Martempering. The steel is quenched into a bath just above the temperature where martensite starts to form, held until the temperature evens out, then air cooled. It reduces distortion and cracking.
- Austempering. The steel is quenched and held at a temperature where bainite forms instead of martensite. The result is tough without a separate tempering step. Austempered ductile iron (ADI) is made this way; see ductile iron.
- Induction and flame hardening. Only the surface is austenitized and quenched, leaving a tough core.
- Double tempering. Tool steels are often tempered twice so that martensite formed from retained austenite during the first temper is itself tempered.
Where Quenched and Tempered Steel Is Used
- High-strength bolts and fasteners
- Shafts, axles, gears, and crankshafts
- Wear plate and high-strength structural plate for cranes and mining equipment
- Pressure vessel and pipeline steels
- Tools, dies, and springs
- Steel castings for heavy equipment, where Q&T replaces normalizing when higher strength is needed
Welding Quenched and Tempered Steel
Q&T steels get their properties from heat treatment, so welding heat can undo them locally. Heat input is kept within limits, and any post weld heat treatment must stay below the original tempering temperature, or the base metal will soften.
Frequently Asked Questions
What is the difference between quenching and tempering? Quenching is rapid cooling that hardens the steel. Tempering is the reheating that follows, which trades a little hardness for a large gain in toughness.
Can every steel be quenched and tempered? No. The steel needs enough carbon, generally about 0.3% or more, to form hard martensite. Low carbon steels respond weakly and are case hardened instead.
Why temper at all? Why not use the steel as quenched? As-quenched martensite is too brittle and too highly stressed for almost any service. A light temper is the minimum for any hardened part.
Is quenching and tempering the same as annealing? No. They are opposites. Annealing cools slowly to make steel as soft as possible. Quenching and tempering cools fast to make it strong.
Conclusion
Quenching and tempering works in three steps: austenitize, quench to martensite, and temper to the required balance of hardness and toughness. Carbon content sets how hard the steel can get, alloy content sets how deep that hardness goes, and tempering temperature sets the final properties.


