
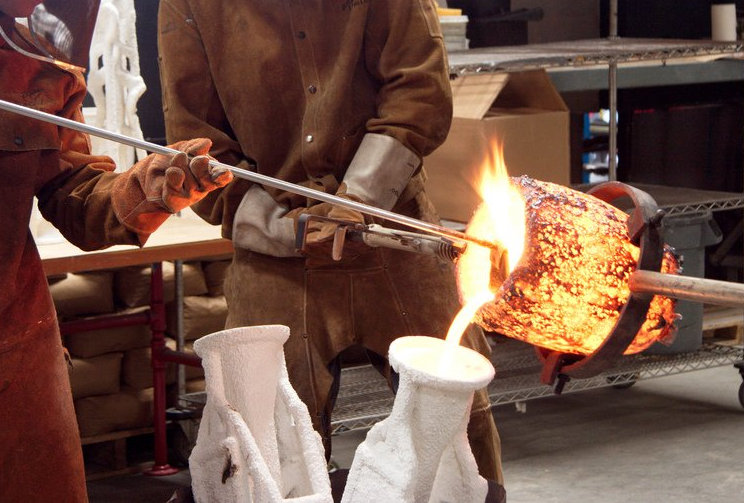
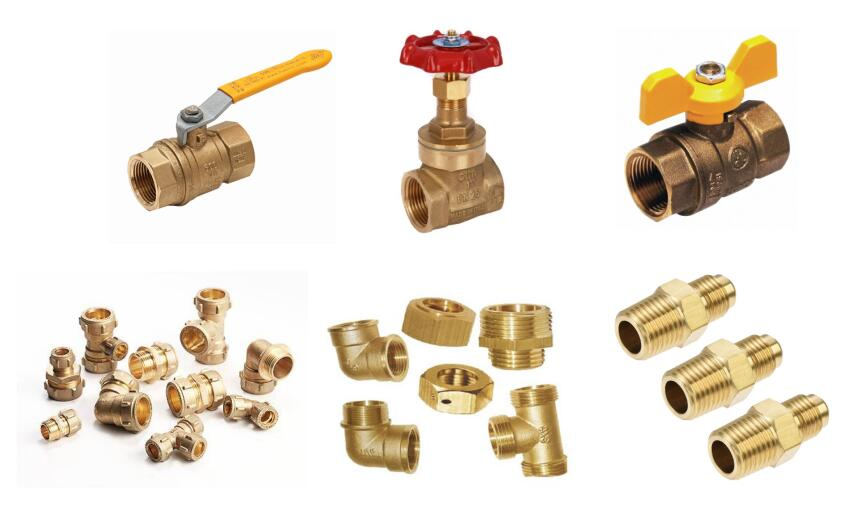
Brass casting is the process of melting a copper-zinc alloy and pouring it into a mold to make parts such as taps, valves, pipe fittings, and decorative hardware. Brass is one of the easier alloys to cast, because it melts at a lower temperature than pure copper and flows well. The main difficulty is zinc, which starts to vaporize at melting temperatures.
This article covers brass specifically. For a comparison with copper and bronze, see our guide to non-ferrous metal casting: copper, brass, and bronze.
Common Cast Brass Types
| Type | Approximate composition | Key properties | Typical products |
|---|---|---|---|
| Red brass | Cu 85%, Zn 5%, Sn 5%, Pb 5% | Pressure tight, resists water corrosion | Valves, fittings, pump housings |
| Yellow brass | Cu 60–70%, Zn 30–40% | Low cost, bright color, easy to cast | Taps, hardware, decorative items |
| High-strength brass (manganese bronze) | Cu-Zn with Mn, Al, Fe | High strength | Propellers, marine components |
| Silicon brass | Cu-Zn-Si | High fluidity, lead-free | Drinking water fittings, precision castings |
Many countries now limit the lead content of components that touch drinking water. As a result, lead-free brasses that use silicon or bismuth instead are increasingly common.
Brass Melting Point and Pouring Temperature
Brass does not melt at a single temperature. It melts over a range, and the more zinc it contains, the lower that range is.
- Melting range: about 900–940°C (1,650–1,725°F) for yellow brass and about 850–1,010°C (1,560–1,850°F) for red brass.
- Pouring temperature: typically about 1,000–1,150°C (1,830–2,100°F) for yellow brass and up to about 1,250°C (2,280°F) for red brass. Thin castings are poured at the upper end of the range, thick castings at the lower end.
- Boiling point of zinc: 907°C (1,665°F). At pouring temperature, the zinc in brass is already inclined to vaporize.
These figures are general ranges. The right temperature depends on the alloy data sheet and the wall thickness of the casting.
Steps in the Brass Casting Process
1. Preparing the charge. Ingots and returns (gates, risers, and scrap from earlier pours) must be dry and free of oil. Damp material is a source of hydrogen gas and can cause a violent reaction when it enters molten metal.
2. Melting. The most common furnaces are gas-fired or oil-fired crucible furnaces and induction furnaces. Melting is done as quickly as possible, with the surface of the melt covered by flux or charcoal to limit oxidation and zinc loss.
3. Correcting the composition. Zinc lost during melting, usually a few percent, is replaced by adding zinc shortly before pouring. In yellow brass, a small amount of aluminum is often added to improve fluidity and suppress zinc vaporization. In red brass, aluminum is avoided because it harms pressure tightness.
4. Skimming. Dross on the surface is removed just before pouring.
5. Pouring. The metal is poured in a calm, unbroken stream. Turbulent pouring drags oxide films into the casting.
6. Shakeout and cleaning. After solidification, the casting is removed from the mold, the gates and risers are cut off, and the surface is cleaned.
Molding Methods Used
- Sand casting: the most common method, suited to small and medium volumes and to large parts.
- Permanent mold (gravity die) casting: used for taps and fittings in large volumes, with a smoother surface.
- Pressure die casting: for small, thin-walled parts in very large volumes.
- Investment casting: for intricate shapes and art castings.
- Centrifugal casting: for cylindrical bushings and bearings.
Common Defects and How to Prevent Them
| Defect | Main cause | Prevention |
|---|---|---|
| Gas porosity | Damp charge, long melting time, excessive temperature | Dry the charge, melt quickly, control temperature |
| Shrinkage cavity | Riser too small or in the wrong position | Recalculate the riser and the solidification direction |
| Dross and zinc oxide inclusions | Dross carried into the mold, turbulent flow | Skim the melt, use a filter, pour calmly |
| Cold shut and misrun | Pouring temperature too low, walls too thin | Raise the pouring temperature, improve the gating |
| Off-composition | Zinc loss not corrected | Add zinc and check with a spectrometer |
How to size a riser against shrinkage cavities is explained in our article on gating and riser system design. How pouring temperature affects mold filling is covered in our article on the fluidity of molten metal.
Safety: Zinc Fumes
Zinc vapor leaving molten brass oxidizes immediately into white zinc oxide fume. Breathing it can cause metal fume fever, with flu-like symptoms that appear a few hours after exposure. Controls include:
- local exhaust ventilation above the furnace and the pouring area,
- melting temperatures that are no higher than necessary,
- a respirator rated for metal fumes,
- extra care with leaded brass, because its fume also carries lead.
Frequently Asked Questions
What is the melting point of brass? About 900–940°C (1,650–1,725°F) for yellow brass. Brasses with more copper melt at higher temperatures.
Why does white smoke appear when melting brass? It is zinc vaporizing and burning to zinc oxide. The smoke shows that zinc is being lost from the alloy, and it is also a breathing hazard.
What is the difference between casting brass and casting bronze? The main alloying element in brass is zinc, while in bronze it is tin. Brass costs less and is easier to machine. Bronze resists wear and seawater better.
Can brass scrap be remelted? Yes, and it is common practice. The scrap needs to be sorted by alloy type and cleaned, and the composition of the melt must be checked, because zinc and lead content can vary.
Conclusion
Brass is relatively easy to cast in terms of temperature and metal flow, but it demands discipline in three areas: fast melting at a controlled temperature, correcting the zinc content before pouring, and good ventilation for zinc fumes. With all three in place, most defects and health risks can be prevented at the furnace.
Related Articles
- Non-Ferrous Metal Casting: Copper, Brass, and Bronze
- Gating and Riser System Design in Metal Casting
- Cold Shut and Misrun Defects in Metal Castings: Causes and Prevention
- 20 Types of Casting Defects: Causes, Identification, and Remedies
- Types of Melting Furnaces for Metal Casting: Induction, Cupola, and Electric Arc


