
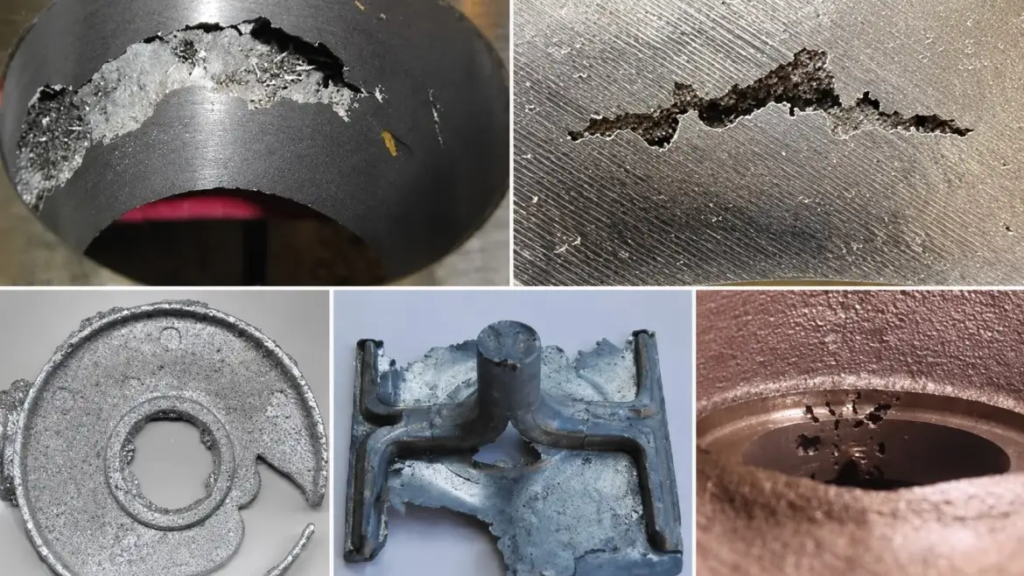
A casting defect is any irregularity that makes a casting fall short of its specification. Some defects are cosmetic and can be ground off. Others, such as internal shrinkage or a hot tear, weaken the part and lead to scrap.
There are dozens of named defects, but almost all of them come from six sources: gas, shrinkage, the mold material, the way the metal is poured, the metallurgy of the alloy, and the alignment of the mold. Grouping defects by source is more useful than memorizing a list, because the source tells you where in the process to look. Types of casting defects, as follows;
The Six Groups at a Glance
| Group | Root cause | Defects covered |
|---|---|---|
| Gas defects | Gas trapped or released in the metal | Gas porosity, blowholes, pinholes |
| Shrinkage defects | Metal contracts as it solidifies | Shrinkage cavity, shrinkage porosity |
| Mold material defects | Sand or coating fails | Sand inclusion, cuts and washes, scab, rat tail and buckle, veining, metal penetration, swell |
| Pouring defects | Metal too cold, too slow, or dirty | Cold shut, misrun, slag inclusion |
| Metallurgical defects | Stress or structure during cooling | Hot tear, hard spots |
| Shape defects | Mold halves or cores out of position | Mismatch and core shift, flash, warpage |
Gas Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 1 | Gas porosity | Small, smooth, rounded voids inside the casting | Dissolved hydrogen or nitrogen released during solidification | Degas the melt, keep charge materials dry, avoid overheating |
| 2 | Blowholes | Larger rounded cavities, often just under the surface | Moisture in the sand, low mold permeability, poor venting | Control sand moisture, add vents, dry cores properly |
| 3 | Pinholes | Many tiny holes, usually under 2 mm, at or near the surface | Hydrogen pickup, wet ladles or tools | Preheat ladles and tools, reduce melt holding time |
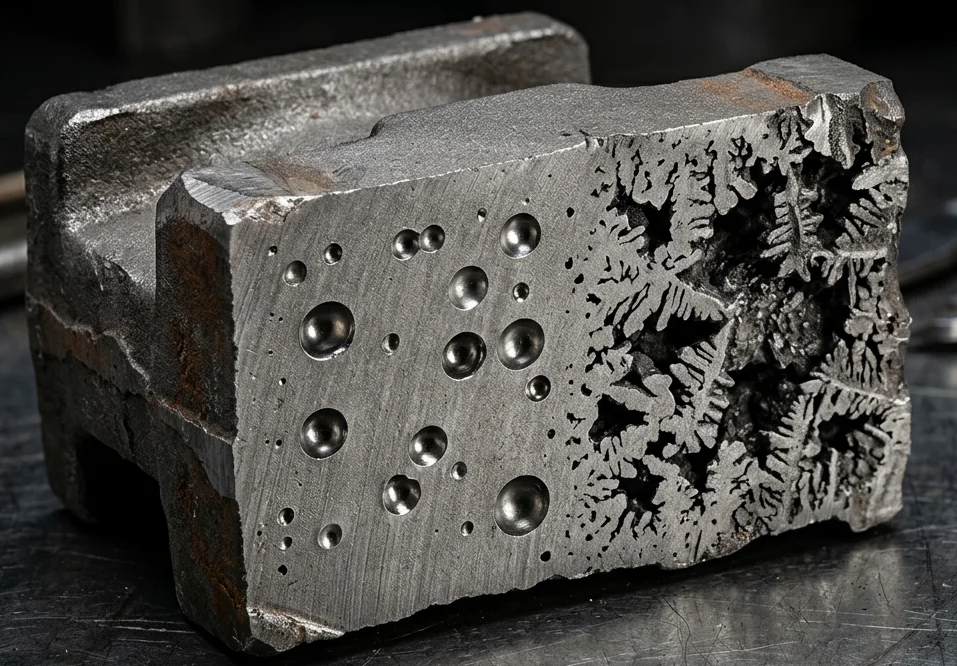
Gas voids have smooth, shiny walls. That is the quickest way to tell them apart from shrinkage voids, which are rough and jagged. Both are covered in more depth in our article on porosity and hot tearing.
Shrinkage Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 4 | Shrinkage cavity | A rough, irregular void, often funnel-shaped, in the last area to solidify | Riser too small or in the wrong place | Resize or relocate risers, promote directional solidification |
| 5 | Shrinkage porosity | A spongy zone of fine, interconnected voids | Long freezing range alloys, isolated thick sections | Add chills, use feeding aids, redesign thick junctions |
Most metals shrink by several percent as they freeze. If liquid metal cannot reach the shrinking area, a void forms. The cure is almost always in the feeding system, as explained in our guide to gating and riser system design.
Mold Material Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 6 | Sand inclusion | Sand grains embedded in the surface or just below it | Weak sand, loose sand left in the mold, erosion | Raise sand strength, blow out molds before closing |
| 7 | Cuts and washes | Raised, rough lumps of extra metal near the gates | Fast metal stream erodes the mold or core | Reduce flow velocity, enlarge or reposition gates |
| 8 | Scab | A thin, rough crust of metal over a layer of sand | Sand expands under heat and the surface layer lifts | Lower sand moisture, add expansion additives, pour faster |
| 9 | Rat tail and buckle | A long shallow line (rat tail) or a deeper V-shaped groove (buckle) | Sand expansion on large flat surfaces | Break up flat surfaces, adjust sand composition |
| 10 | Veining | Thin fins of metal standing up from a cored surface | Cores crack as silica sand expands | Use anti-veining additives or lower-expansion sands |
| 11 | Metal penetration | A rough, sandpaper-like surface with sand fused in | Coarse sand, soft ramming, pouring too hot | Use finer sand, compact harder, apply mold coating |
| 12 | Swell | A local bulge that makes the casting oversize | Mold wall moves under metal pressure | Ram the mold harder, support the flask |
Pouring Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 13 | Cold shut | A line or seam where two metal streams met but did not fuse | Low pouring temperature, slow filling, thin sections | Pour hotter and faster, add gates, improve venting |
| 14 | Misrun | An incomplete casting with rounded, unfilled edges | Metal froze before filling the cavity | Same as cold shut, plus thicker sections where possible |
| 15 | Slag inclusion | Irregular non-metallic particles, usually on upper surfaces | Slag or dross carried into the mold | Skim the ladle, use filters and slag traps |
Cold shuts and misruns share the same root cause: the metal ran out of heat before it finished its job. See cold shut and misrun casting defects for the full treatment, and inclusion defects in metal casting for slag, dross, and oxide films.
Metallurgical Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 16 | Hot tear | A ragged, branching, oxidized crack | The casting is restrained while it is still weak and shrinking | Use collapsible cores, add fillets, avoid abrupt section changes |
| 17 | Hard spots | Very hard, unmachinable areas in gray iron, white when fractured | Thin sections cool too fast, poor inoculation | Improve inoculation, adjust composition, thicken thin edges |
Shape Defects
| # | Defect | What it looks like | Main causes | Remedies |
|---|---|---|---|---|
| 18 | Mismatch and core shift | A step at the parting line, or uneven wall thickness | Worn pins, misaligned flask halves, cores that float | Maintain pins and bushings, anchor cores with chaplets |
| 19 | Flash | A thin fin of metal along the parting line | Mold halves not clamped tightly, worn patterns | Clamp or weight the mold, repair patterns |
| 20 | Warpage | The casting is bent or twisted | Uneven cooling and residual stress | Balance section thickness, stress relieve after casting |
How Casting Defects Are Found
- Visual inspection catches surface defects such as flash, mismatch, scabs, and cold shuts.
- Dimensional checks catch swell, warpage, and core shift.
- Non-destructive testing finds what the eye cannot. Radiography reveals internal porosity and shrinkage, ultrasonic testing finds internal cracks, and penetrant or magnetic particle testing reveals fine surface cracks. See NDT methods for metal casting.
- Automated inspection with machine vision is increasingly used on high-volume lines, as described in AI casting defect detection.
Preventing Defects Before Pouring
Most defects are designed in long before the metal is melted. Three practices prevent the majority of them:
- Design the part for casting. Uniform walls, generous fillets, and gradual transitions remove the hot spots where shrinkage and hot tears start.
- Simulate filling and solidification. Digital simulation shows where metal will arrive cold or freeze last, before any tooling is cut.
- Control the process variables. Pouring temperature, sand moisture, and melt cleanliness account for a large share of day-to-day scrap.
Frequently Asked Questions
What is the most common casting defect? Porosity, in its gas and shrinkage forms, is generally regarded as the most frequent cause of rejected castings, especially in aluminum.
Can casting defects be repaired? Many can. Surface defects are ground out, and some cavities and cracks are repaired by welding when the specification allows it. See repair welding of metal castings.
How do I tell gas porosity from shrinkage porosity? Look at the walls of the void. Gas pores are smooth and rounded. Shrinkage voids are rough, angular, and often show a dendritic texture.
Are all defects grounds for rejection? No. Acceptance depends on the standard and the customer’s requirements. A defect that is acceptable in a counterweight may be unacceptable in a pressure-containing valve body.
Conclusion
The twenty defects above fall into six groups, and each group points to a different part of the process: the melt, the feeding system, the sand, the pour, the alloy, or the mold assembly. Identifying the group first is the fastest route to the cause, and fixing the cause is always cheaper than sorting out bad castings afterward.


